Why an Approved Sample Does Not Prove Bulk Custom Drinkware Will Match It
Key procurement answer
An approved sample is valuable visual and functional evidence, but it does not prove that normal bulk production will use the same configuration, materials, components, tooling, process conditions, or acceptance controls. This guide explains the evidence bridge that turns sample approval into a defensible production decision.
Procurement position: An approved custom drinkware sample proves that one identified unit was acceptable when it was reviewed. It does not, by itself, prove that a normal bulk-production run will use the same material and component sources, artwork revision, tooling, operators, process settings, assembly conditions, or acceptance controls. The stronger approval decision creates an evidence bridge between the approved requirement, a production-intent sample, the conditions used for bulk manufacture, and the records used to release the delivered order. Without that bridge, a buyer may have an attractive reference unit but no reliable basis for deciding whether the quantity produced is genuinely the same product.
This distinction is easy to miss because a physical sample feels conclusive. A buyer can hold it, inspect the colour, test the lid, compare the logo placement, check the capacity, and show it to an internal stakeholder. That is useful evidence. It establishes what the buyer considers acceptable for that particular unit. The error begins when the sample is treated as proof of a future process rather than as a reference that the future process must be connected to. A bottle that looks correct before a production schedule is released has not yet demonstrated that repeat production can preserve the same configuration under normal operating conditions.
A sample answers a unit-level question; bulk production creates a system-level question. The sample can answer whether the visible item has an acceptable shape, finish, decoration, fit, feel, and function at the time of review. Bulk production asks whether a manufacturing system can repeatedly deliver that outcome across a defined order. The difference includes the number of units, the origin of materials and components, the equipment and tooling in use, the people carrying out the work, the production speed, the inspection approach, and the possibility that a commercial constraint changes one of those inputs. A single acceptable unit should therefore be treated as a benchmark, not a substitute for evidence that the bulk system can meet the benchmark.
The U.S. Food and Drug Administration’s process-validation guidance is written for pharmaceutical manufacture, not drinkware, and it does not regulate a corporate bottle order. Its evidence logic is nevertheless useful as a bounded manufacturing analogy. It defines validation as collecting and evaluating data from process design through commercial production to establish that a process can consistently deliver quality. It distinguishes defining a process, qualifying whether it can reproduce a commercial result, and continuing to verify control during routine production. The relevant lesson for a drinkware buyer is not to copy a regulated-industry protocol. It is to avoid treating an early unit as if it were evidence from the conditions that will make the order.
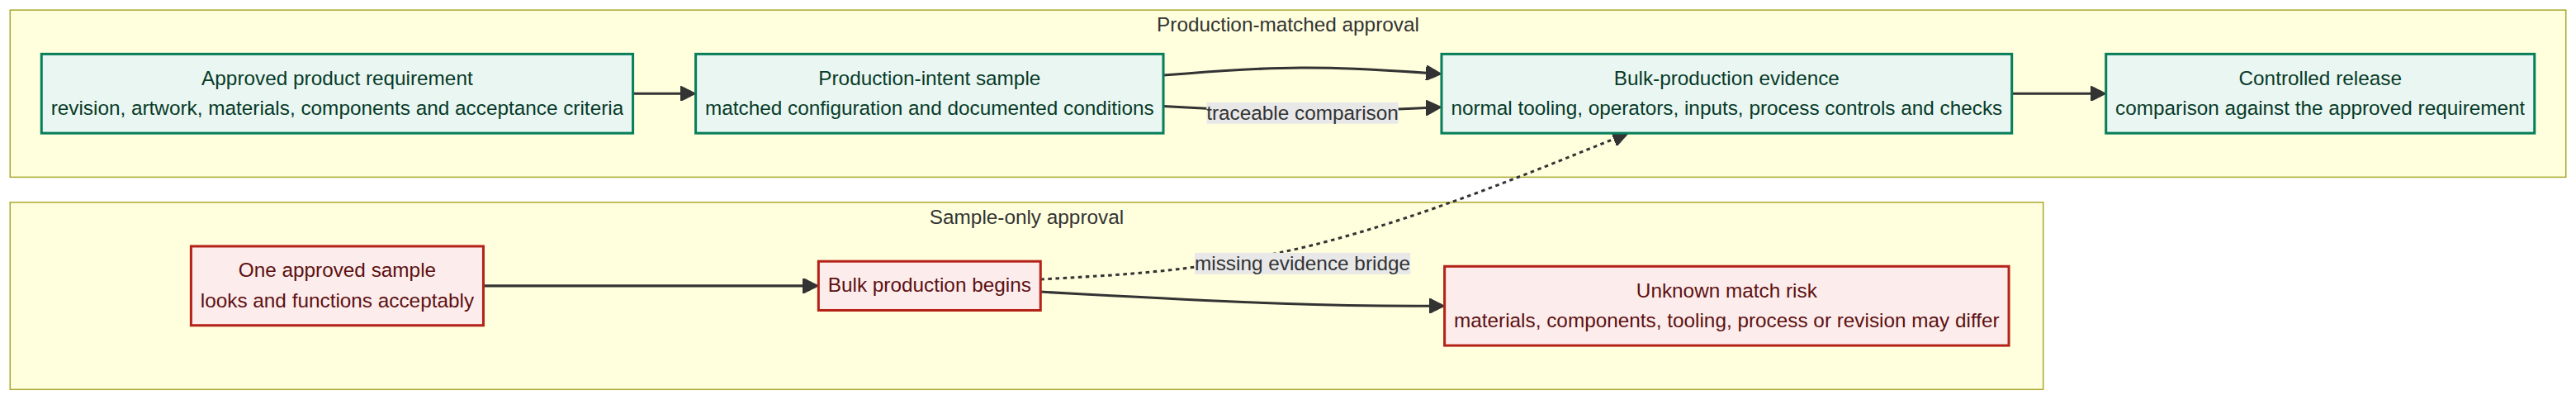
The diagram separates the two approval paths. In the sample-only path, bulk production begins after one acceptable unit, leaving an untested gap between the sample and the normal production conditions. In the production-matched path, the approved product requirement identifies the revision, artwork, materials, components, and acceptance criteria; a production-intent sample records the matched configuration; bulk evidence records the normal inputs and controls; and release compares the delivered population against that same requirement. The purpose is not to require every buyer to run a formal validation programme. It is to preserve the links that make a sample relevant to the quantity being purchased.
The governing requirement must be identifiable before the sample can become a benchmark. A sample can only be compared with later production if both are tied to a controlled description of the product. For custom drinkware, that description may include the product reference, capacity, body finish, colour standard, artwork file and placement, decoration method, lid and gasket configuration, packing requirement, intended use, and defined acceptance checks. If the buyer approves a sample based on a gallery of images, a chat message, and a general product name, the factory may have no single reference that tells production or inspection which details were essential and which were merely illustrative.
The International Organization for Standardization explains that ISO 9001 is a framework for delivering consistent products and services through a process approach, risk-based thinking, documented information, monitoring, measurement, and continual improvement. The overview does not say that a drinkware supplier is certified or that one procedure fits every order. It does reinforce the practical point that consistency depends on defining the process and using evidence about its performance, not on relying on memory of a prior unit. The approved sample is strongest when it is attached to the same version-controlled requirement that production and inspection will use.
“Production-intent” matters more than “first sample” when the buyer is trying to reduce mismatch risk. A presentation sample may have been made slowly by an experienced technician, with hand-selected components, preliminary artwork, an early tooling setup, or a finish that was available only for that trial. None of those facts makes the sample misleading. They simply limit what it can prove. A production-intent sample is more informative when the buyer knows whether it used the proposed body and closure configuration, decoration system, artwork revision, key material and component sources, tooling route, and packing method that are intended for the order. The closer those conditions are to the normal run, the more relevant the sample comparison becomes.
Scale can introduce variation even when the design has not changed. The National Institute of Standards and Technology notes, in its additive-manufacturing process-control work, that part quality is highly dependent on process control and that apparently comparable strategies can produce different build quality where implementation differs. The technical setting is additive manufacturing, not beverage containers, so it should not be read as a claim about a particular bottle factory. The transferable principle is straightforward: a nominal design does not eliminate variation created by process execution. For drinkware, differences can arise through surface preparation, printing or curing conditions, closure assembly, incoming component batches, fixture wear, packing sequence, or inspection interpretation.
Acceptance criteria should translate the sample into checks that another person can perform. “Match the approved sample” may be a useful instruction, but it is incomplete where different people could interpret it differently. The inspection record should identify the features that are material to release: for example, the applicable artwork revision and location, colour or finish reference, capacity or key dimensions, lid engagement, leak check, component completeness, visible-defect boundary, and packing configuration. Each feature does not need the same test method. The point is to turn the approved reference into observable conditions and a clear basis for accepting, holding, or investigating a bulk lot.
The FDA guidance provides a useful illustration of this evidence design without setting a drinkware requirement. It describes written protocols that specify manufacturing conditions, material inputs, data collection, tests, acceptance criteria, sampling, performance indicators, and how deviations are handled. A proportionate drinkware order may use a much simpler record, but the logic remains valuable. If a colour drift, lid fit issue, logo-placement variation, or packing change occurs, the buyer and supplier should be able to determine whether it was within the agreed acceptance basis, whether it affected the population released, and whether a revised decision is needed.
First-off or early-run comparison closes a gap that pre-production review cannot see. A sample made before normal production may confirm design intent. An early production comparison can reveal whether the line, tooling, inputs, and work instructions are delivering that intent in the actual run. This comparison is especially useful where the order includes multiple components, a sensitive decoration process, a new finish, a tight packing constraint, or a recipient-facing product that will be judged visually. The buyer does not need to prescribe the factory’s internal workflow. It is enough to agree which characteristics will be compared, which evidence will be retained, and who can decide whether a detected difference is acceptable before the order advances.
The comparison should also be traceable to the produced population. If the supplier changes a lid source after the sample, moves a decoration process, replaces a coating, revises the artwork, or introduces a new packaging component, the sample approval cannot automatically follow the changed configuration. The earlier custom drinkware customization process provides the broader sequence for linking artwork, product configuration, sample review, production, inspection, and delivery. Within that sequence, the practical rule is simple: when the configuration or evidence basis changes, compare the changed item against the governing requirement before treating the original sample approval as still applicable.
Release evidence should state what was compared, not merely that the order was approved. A release record gains value when it identifies the order and product revision, the production lot or run, the approved reference, the checks completed, the inspected population or sampling basis, the result, and any authorized deviation. A simple statement such as “sample approved” is weak once a dispute occurs because it does not reveal whether the sample had the same lid, finish, print, component lot, or packing configuration as the production population. A more specific record helps a buyer distinguish a genuine production departure from a feature that was knowingly accepted.
The commercial consequence of skipping this bridge is often delayed rather than immediate. The delivered units may appear acceptable at receiving but show inconsistent logo appearance across offices, different closure feel across a gift programme, fit problems in pre-assembled event kits, or replacement requests when a component behaves differently in use. The procurement file then contains a sample that everyone remembers approving but few records that explain how the delivered item was compared with it. That makes containment, supplier discussion, and future reorders more difficult than they need to be.
A proportionate request is therefore practical: identify the approved product revision; retain the production-intent sample or its controlled record; disclose any material, component, artwork, finish, tooling, process, or packing difference that could affect the buyer’s requirements; compare the early production output against the agreed acceptance criteria; record the applicable lot or run; and document any approved exception. The level of detail should match the risk of the order. A simple one-colour event cup does not require the same evidence depth as a multi-component insulated bottle for daily staff use. Both, however, benefit from separating a one-unit approval from evidence that the released population matches it.
An approved sample remains one of the most useful decisions in custom drinkware procurement. It establishes a tangible reference, exposes visible expectations early, and can prevent a design error from reaching bulk production. Its value is reduced only when it is asked to prove more than it can. The defensible question is not “Was a sample approved?” It is “Can the supplier show that the approved requirement, production-intent configuration, normal bulk conditions, inspection evidence, and released lot are connected?” When the answer is yes, sample approval becomes part of a controlled production decision rather than a hopeful memory of what one unit looked like.