Why a Digital Artwork Proof Does Not Prove Custom Drinkware Colour Will Match Production
Key procurement answer
A digital artwork proof confirms a version, placement, and intended appearance on a specified screen or proofing context. It does not by itself prove that the final bottle, tumbler, cup, or mug will reproduce the same perceived colour. This guide explains how to connect digital approval with a physical production reference.
Procurement position: A digital artwork proof confirms that a specified artwork revision, logo location, wording, and intended visual appearance were approved in a particular digital context. It does not by itself prove that a printed, coated, engraved, or otherwise decorated bottle, tumbler, cup, or mug will reproduce the same perceived colour in physical production. A reliable colour decision links the approved artwork to a defined colour reference, the actual drinkware substrate and decoration process, and an agreed physical comparison or measurement basis before the order is released.
This gap is easy to overlook because the proof is often the most visible approval step. A marketing team receives a PDF or on-screen mock-up, checks the logo spelling and position, and confirms that the brand colour looks right on a laptop display. That is worthwhile. It prevents an outdated logo, incorrect placement, or obvious artwork error from reaching production. The mistake is asking the same digital image to prove something it was not designed to prove: how a particular ink, coating, or finish will appear on a curved physical object under real viewing conditions.
Digital approval and physical colour approval answer different questions. The digital proof answers whether the correct design file and intended appearance have been selected. Physical colour approval answers whether a defined decoration process on the actual body and finish produces an acceptable result against an agreed reference. Those questions overlap, but they are not interchangeable. A logo can be perfectly positioned and use the correct file while its physical result appears lighter, darker, warmer, cooler, less saturated, or less even than the viewer expected from the screen.
The International Organization for Standardization describes ISO 12647-7:2016 as requirements for hard-copy digital proof systems intended to simulate a printing condition defined by characterisation data, with recommendations for appropriate test methods. ISO confirms that the 2016 edition remains current after its 2022 review. The standard concerns graphic-technology proofing, not drinkware decoration, and it should not be presented as a requirement for a branded bottle order. Its useful transferable principle is narrower: a proof is a controlled simulation of a defined output condition. It is not an unconditional promise that every later physical process or substrate will look identical.
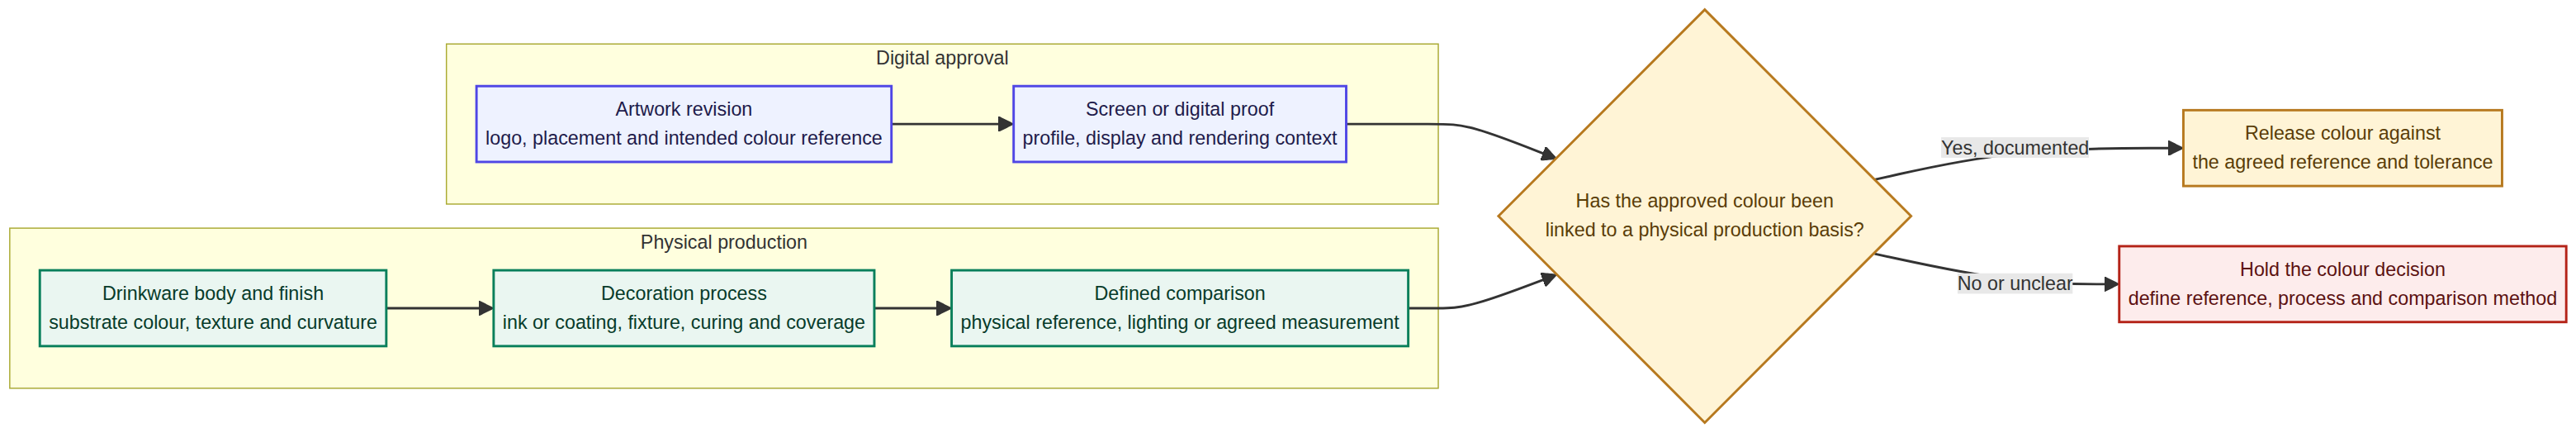
The diagram separates the two paths. The digital side records the artwork revision and the screen or proofing context in which intended colour was viewed. The physical side records the body and finish, the decoration process, and the agreed method for comparing the result. The decision is not whether the supplier supplied a proof; it is whether the approved colour has been connected to a physical production basis. When that connection is documented, the colour can be released against an agreed reference and tolerance. When it is not, the right next step is to define the reference, process, and comparison method—not to assume the screen will settle the disagreement later.
A colour name or code is useful, but it is not a complete production instruction. A named brand colour, RGB value, CMYK build, or spot-colour reference can communicate design intent. It may not define the result on every substrate or through every decoration process. For a drinkware order, the procurement file should clarify which reference is governing: a physical colour chip, a retained physical sample, a named standard under a stated lighting condition, a measured target with an agreed tolerance, or another reference that the buyer and supplier can both access. If the order relies only on “match the artwork,” two reasonable people may still be comparing different things.
The International Color Consortium explains why this happens across digital workflows. Its colour-management guidance describes the transformation of data from one device, such as scanner RGB, to another, such as printer CMYK. ICC profiles define the relationship between a device’s digital values and a standard colour space, and applying colour management requires profiles for the relevant input and monitor or printing device. A custom drinkware supplier does not need to operate an ICC workflow for this point to matter. The practical lesson is that digital file values, display colour, and physical output are not automatically the same reference; they need a defined translation or comparison method.
The actual body is part of the colour system. A print placed on a white gloss bottle can look different on a black powder-coated tumbler, a coloured plastic cup, a brushed metal surface, or a ceramic glaze. The base surface affects what the viewer sees through opacity, reflectance, texture, and contrast. A supplier may use an underbase, multiple passes, a different ink sequence, or another process adjustment to reach an acceptable appearance. Those controls can be appropriate, but they should be recognised as part of the approved production configuration. When the body finish, base colour, or decoration route changes, the original digital proof cannot automatically be treated as a complete colour approval for the changed product.
A physical pre-production sample can therefore add evidence that a screen proof cannot provide. It lets the buyer view the actual substrate, decoration coverage, logo edge quality, registration, finish, and perceived colour together. Yet a physical sample should still be identified precisely. A useful record states the product revision, body finish and colour, artwork revision, decoration method, location, date, and any agreed colour reference. If it is being used as a colour master for bulk production, it should be retained or photographed with enough controlled context that a later inspector knows what it represents. “Sample approved” is weaker than “sample approved as the colour and placement reference for artwork revision X on body finish Y using decoration process Z.”
Fogra’s Contract Proof Creation programme makes the value of named conditions visible in the graphic-arts setting. It describes a colour-accurate proof as a visual reference under ISO 12647-7 and requires information including the substrate material type, the simulated printing condition, production time and date, and the measurement condition. Its procedure examines the substrate as well as measured colour accuracy, gamut, gray balance, uniformity, and tone-value reproduction. Fogra does not certify a drinkware-decoration process, and its proof programme is not a buyer requirement for branded cups. It does illustrate why a useful reference identifies the conditions under which it is meaningful rather than relying on a generic “colour approved” label.
Viewing conditions should be agreed before a marginal difference becomes a dispute. A colour may look different in daylight, warm office lighting, a warehouse, or under a phone camera. A physical review can also be affected by angle, gloss, shadow, and the proximity of other colours. The order does not need a laboratory-grade measurement programme for every one-colour giveaway cup. It does need an acceptance basis proportionate to the brand and order risk. That may be an agreed physical master sample viewed in neutral lighting, a named colour target with a supplier-defined tolerance, or a documented instrument comparison for a sensitive corporate identity. The important point is to choose the basis before mass production, not after a delivery has been unpacked.
This record becomes especially valuable at reorder or change points. A body supplier may alter a finish, a decoration location may move to another line, a new ink system may be introduced, or an artwork file may be converted through different software. None of these changes automatically makes the product unacceptable. Each can change the relevance of a previous physical colour reference. The buyer should ask whether the governing colour reference still matches the proposed body and process, what comparison will be performed, and whether the original approval applies unchanged, applies with a documented qualification, or needs a new reference. That is a targeted decision, not a request to repeat every approval step without reason.
A concise colour-control brief can make the decision repeatable. It identifies the order and product revision; artwork revision; logo location; intended colour reference; body material and finish; decoration method; physical sample or production condition where applicable; agreed viewing or measurement basis; who may approve a deviation; and the retained record. It does not need to expose a supplier’s proprietary process settings. It gives both sides enough shared language to determine whether the first-off output and later lot remain within the agreed appearance boundary.
The right place for this control is inside the custom drinkware customization process, alongside product selection, artwork revision approval, sample review, production control, and release. The file can be approved digitally to lock the content and placement. The physical colour can then be confirmed on the specified product configuration through the agreed reference. If a change occurs, compare it against that same basis before releasing the affected units. This sequence keeps creative approval fast while preserving a clear path for resolving the separate physical-production question.
A digital artwork proof is indispensable for managing design intent. Its value is reduced only when it is asked to prove more than a digital approval can show. For custom drinkware, the practical question is not “Was the logo proof approved?” It is “Which physical colour reference, product surface, decoration process, and comparison condition connect that approved artwork to this production run?” When that question is answered before release, the buyer has a usable basis for acceptance and the supplier has a clearer, more repeatable target for production.